Welcome! Please use the navigational links to explore our website.
PartsASAP LogoCompany Logo (800) 853-2651

Shop Now

   Allis Chalmers Case Farmall IH Ford 8N,9N,2N Ford
   Ferguson John Deere Massey Ferguson Minn. Moline Oliver

Attention Forum Users: On the 28th of December 2023 at 9:00am Central Time, we will be taking the forums down for maintenance while we prepare the new forums for your use. Please click here for more information.

Tool Talk Discussion Forum

welding rods

Welcome Guest, Log in or Register
Author 
james braley

04-06-2007 16:44:18


Report to Moderator

a freind told me i should start useing 7018 Ac instead of 6011 whats the diference.


[Log in to Reply]   [No Email]
james braley

04-07-2007 06:40:05


Report to Moderator
 Re: welding rods in reply to james braley, 04-06-2007 16:44:18  
thanks guys for all the info. bought some 7018 last night and started welding and i guse im braggen but i have never welded preteir. (i have always used 6011)


[Log in to Reply]  [No Email]
MarkB_MI

04-07-2007 06:16:20


Report to Moderator
 Re: welding rods in reply to james braley, 04-06-2007 16:44:18  
6011 is a much more versatile rod than 7018. It has deep penetration and will penetrate rust and paint. It has fast-freeze characteristics, meaing that the bead solidifies quickly. 6011 is pretty much immune to moisture and doesn't have any special storage requirements. 6011 makes welds that aren't very pretty but have good penetration.

7018 is a "low-hydrogen" rod intended for making high-strength welds on clean metal. It has medium penetration. It is considered to be a fill-freeze rod and makes a good-looking weld. This biggest problem with 7018 is that it is susceptible to moisture and needs to be stored properly in humid climates.

Another rod to consider is 7014, which is a very easy rod to use on clean metal, and makes a nice weld with medium penetration.

If I could only use one of the above rods, I think it would have to be 6011.

[Log in to Reply]  [No Email]
135 Fan

04-07-2007 09:15:10


Report to Moderator
 Re: welding rods in reply to MarkB_MI, 04-07-2007 06:16:20  
As long as 7018 are stored in a dry location, they are fine. You can get rod keepers with screw on lids to store them. Unless you're doing X-ray quality welds you don't need a rod oven. Most people that do welding have a grinder and/or a wire brush. The key to getting a good weld is to have the steel as clean as possible with the proper joint preperation and fit up. Although 7018 doesn't penetrate as much as 6011 it builds up more. A 7018 pass could hold together better than a 6011 because 6011 leaves a flat bead profile. 6011 would be good on a butt weld with no gap. On a fillet weld 7018 would be a lot stronger. For the same penetration 7018 would also be a lot stronger than 7014. Dave

[Log in to Reply]  [No Email]
TomTX

04-07-2007 19:33:53


Report to Moderator
 Re: welding rods in reply to 135 Fan, 04-07-2007 09:15:10  
If memory serves me correctly, 7014 rod has 70,000 lbs which is what the first 2 digits of the number means; i.e. 7014, 7018, etc. Tom


[Log in to Reply]  [No Email]
lucasss

04-07-2007 05:40:47


Report to Moderator
 Re: welding rods in reply to james braley, 04-06-2007 16:44:18  
we use 6011 and 6013 on cold roll steel. 7018 we use on high carbon steel, you know,the tough steel.never let me down. lucas


[Log in to Reply]  [No Email]
TomTX

04-07-2007 05:14:48


Report to Moderator
 Re: welding rods in reply to james braley, 04-06-2007 16:44:18  
James, go to lincoln electric on the net and look at ord specs. It shows you the breakdown of the rod numbers. I agree with Old, on fairly clean steel around the farm I use mostly 7014 rod in the 1/8 size. Use some 7014 in 5/32 for heavy welds. Use some 7014 in 3/32 for small welds. Use some 6011 for dirty, rusted stuff. Seldom use 7018, partly because of my skill level. Tom


[Log in to Reply]  [No Email]
mph

04-06-2007 21:28:38


Report to Moderator
 Re: welding rods in reply to james braley, 04-06-2007 16:44:18  
I myself as a rule use 6011 and 7018 depending on app. sometimes together, my personal stance on any stick welding is the 7018. Master that and you will have a good weld all the way around.


[Log in to Reply]  [No Email]
old

04-06-2007 19:08:20


Report to Moderator
 Re: welding rods in reply to james braley, 04-06-2007 16:44:18  
My self I use a lot of 7014 rod, 7018 can be a little hard to work with and if your useing an AC machine it gets to be even harder to use. All depends on what your welding as to what rod you use.


[Log in to Reply]  [No Email]
mjbrown

04-06-2007 17:20:39


Report to Moderator
 Re: welding rods in reply to james braley, 04-06-2007 16:44:18  
6011 is a quick freeze rod. It solidifies before bubbles can travel up through it and cause leaks in pipe welds. 7018 is a low hydrogen rod used where hydrogen embrittlement might be a problem in some steels. I saw that useing old discs for pedestal bases. The 6013 beads popped right out of the base metal as they cooled. When I switched to 7018 and preheated they held fine.
I think 6011 has it's uses. No rod is right for all circumstances.

[Log in to Reply]  [No Email]
mj

04-06-2007 17:12:19


Report to Moderator
 Re: welding rods in reply to james braley, 04-06-2007 16:44:18  
6011 is a fast-freeze, deep-penenetration AC rod which, as was said, works well over rust, paint, etc. It has a yield strength of 50,000psi. 7018 is a 'low-hydrogen rod' which runs best on DC RP or AC w/Hi-freq. arc stabilization. It has a yield strength of 70,000psi. & is my choice for truck frames, high-tensile strength implement repair, etc.


[Log in to Reply]  [No Email]
135 Fan

04-06-2007 22:35:23


Report to Moderator
 Re: welding rods in reply to mj, 04-06-2007 17:12:19  
High frequency is only used for TIG welding. 6011 has a minumum tensile strength of 60,000 psi hence the "60". 6011 is a deep penetrating rod but doesn't fill in a lot. 7018 is the best all around rod to use if you want something to be strong. They take practice to use on an AC machine. If you have dirty steel use a 6011 and cover it with a 7018 if you want maximum strength. It is common for pressure piping and vessels to use a 6010 root pass with 7018 fill and cap. If you are welding other things than pipe and you need the most strength, you can use the same technique. Dave

[Log in to Reply]  [No Email]
mj

04-07-2007 20:44:50


Report to Moderator
 Re: welding rods in reply to 135 Fan, 04-06-2007 22:35:23  
third party image

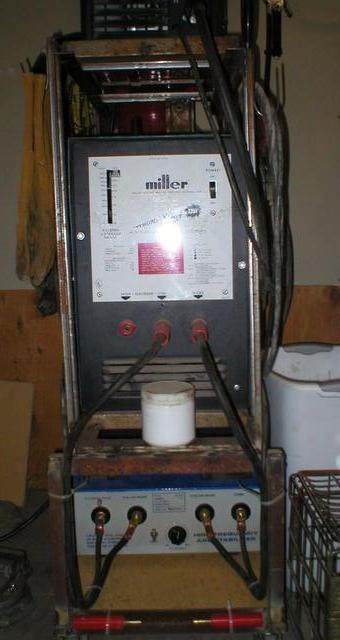
You said - "6011 has a minumum tensile strength of 60,000 psi hence the "60". I said: "It has a yield strength of 50,000psi." Yield not tensile. You said: "High frequency is only used for TIG welding." I say: "Have you ever tried it?"

[Log in to Reply]  [No Email]
Frank Slater

04-06-2007 16:54:52


Report to Moderator
 Re: welding rods in reply to james braley, 04-06-2007 16:44:18  
6011 are for rusty & thin metal. 7018 are for hard metal like drill stem pipe & sucker rod.


[Log in to Reply]  [No Email]
135 Fan

04-06-2007 22:40:15


Report to Moderator
 Re: welding rods in reply to Frank Slater, 04-06-2007 16:54:52  
About the only thing drill stem (that's magnetic) and sucker rod is good for is a fence. It is not really considered a weldable steel for anything structural. You can weld thicker sections with 6011 but you need more passes. Dave


[Log in to Reply]  [No Email]
[Options]  [Printer Friendly]  [Posting Help]  [Return to Forum]   [Log in to Reply]

Hop to:


TRACTOR PARTS TRACTOR MANUALS
We sell tractor parts!  We have the parts you need to repair your tractor - the right parts. Our low prices and years of research make us your best choice when you need parts. Shop Online Today. [ About Us ]

Home  |  Forums


Copyright © 1997-2023 Yesterday's Tractor Co.

All Rights Reserved. Reproduction of any part of this website, including design and content, without written permission is strictly prohibited. Trade Marks and Trade Names contained and used in this Website are those of others, and are used in this Website in a descriptive sense to refer to the products of others. Use of this Web site constitutes acceptance of our User Agreement and Privacy Policy

TRADEMARK DISCLAIMER: Tradenames and Trademarks referred to within Yesterday's Tractor Co. products and within the Yesterday's Tractor Co. websites are the property of their respective trademark holders. None of these trademark holders are affiliated with Yesterday's Tractor Co., our products, or our website nor are we sponsored by them. John Deere and its logos are the registered trademarks of the John Deere Corporation. Agco, Agco Allis, White, Massey Ferguson and their logos are the registered trademarks of AGCO Corporation. Case, Case-IH, Farmall, International Harvester, New Holland and their logos are registered trademarks of CNH Global N.V.

Yesterday's Tractors - Antique Tractor Headquarters

Website Accessibility Policy